PEEK does not reward improvisation. These six design decisions account for most of the difference between a tool that runs and a tool that keeps being adjusted.
| Design area | What we specify |
|---|---|
| Steel selection | S136 / STAVAX corrosion-resistant or H13 hot-work steel; critical parts vacuum hardened and cryogenically treated to HRC 52–56, with TiN or chrome plating on contact surfaces. |
| Gating | Large gates and short runners; hot-runner or semi-hot-runner preferred. Gate size runs 30–50 % larger than for commodity plastics to keep shear down. |
| Temperature control | Mold-face temperature difference within ±2 °C — the number-one cause of warpage. Cooling channels 8–12 mm diameter at 15–20 mm pitch, conformal where geometry allows. Moving half, fixed half, core and cavity on independent circuits. |
| Venting | Vents 0.015–0.02 mm deep and 5–10 mm wide, placed at the end of fill, at weld lines and in deep pockets. At PEEK's fill speed, poor venting shows up immediately as burns or weak weld lines. |
| Ejection | Draft from 1.5° on standard parts and 0.5° on precision features; cavity walls 1.8–3°; variable draft in deep parts. Ejector pins ≥ 3 mm diameter at ≤ 80 mm pitch, stripper plate or air ejection for thin-wall deep parts. Ejection hardware TiN coated (friction coefficient ≤ 0.18) and polished in the ejection direction. |
| Tolerance control | Molded part tolerance target ±0.02 mm; mold component tolerance ±0.02–0.001 mm; parting-line contact gap ≤ 0.02 mm. Key dimensions under SPC with CPK ≥ 1.33. |
Maximum mold-face temperature difference. Uneven mold temperature is the number-one cause of warpage.
Vent depth. At PEEK fill speeds, too little venting shows up as burns and weak weld lines.
Target tolerance on molded parts, with mold components held to ±0.02–0.001 mm.
Minimum CPK on key dimensions, monitored under SPC.
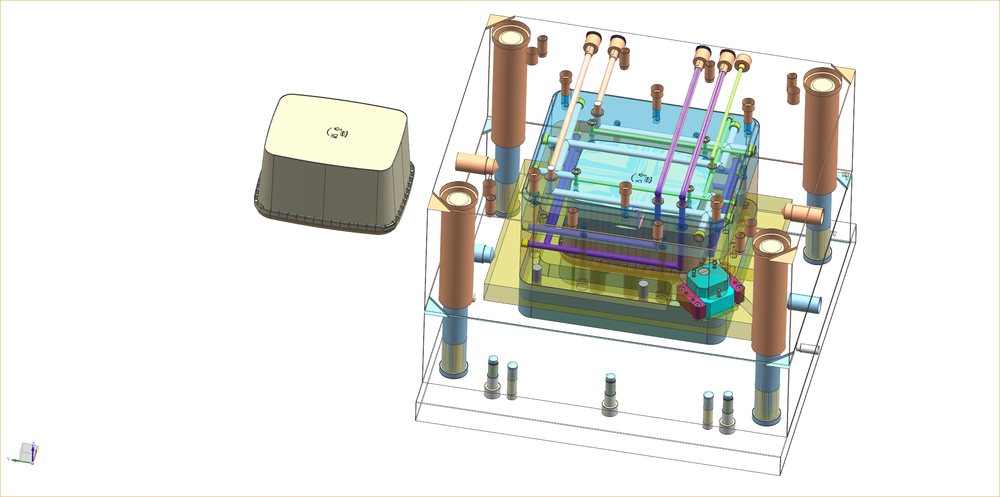
Give us the part and we return a complete design package — not a price alone:
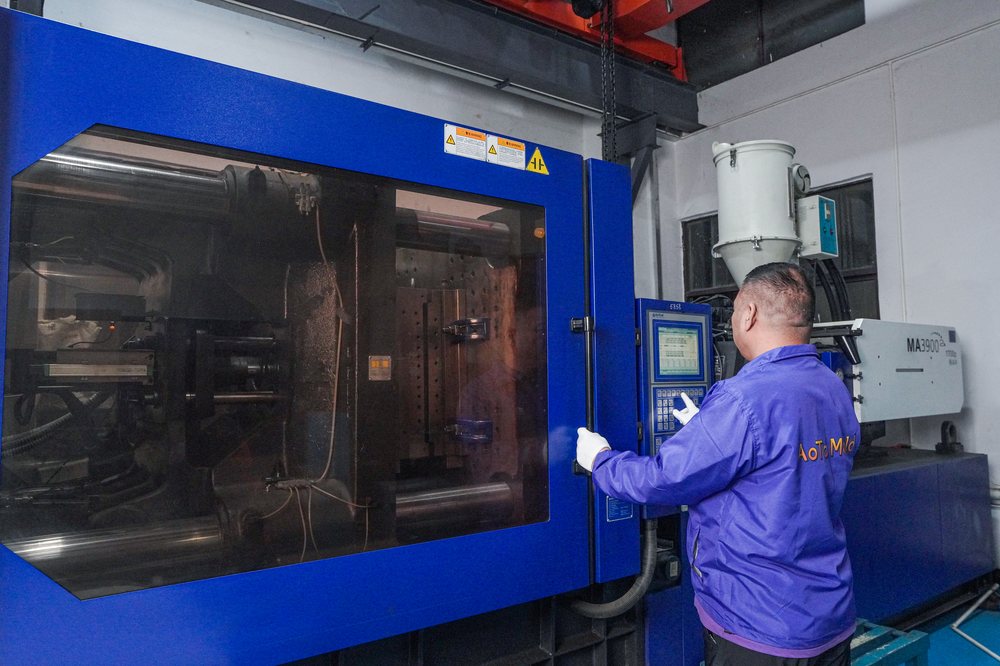
Drying, barrel and mold temperatures, annealing, and a defect troubleshooting table.
Read more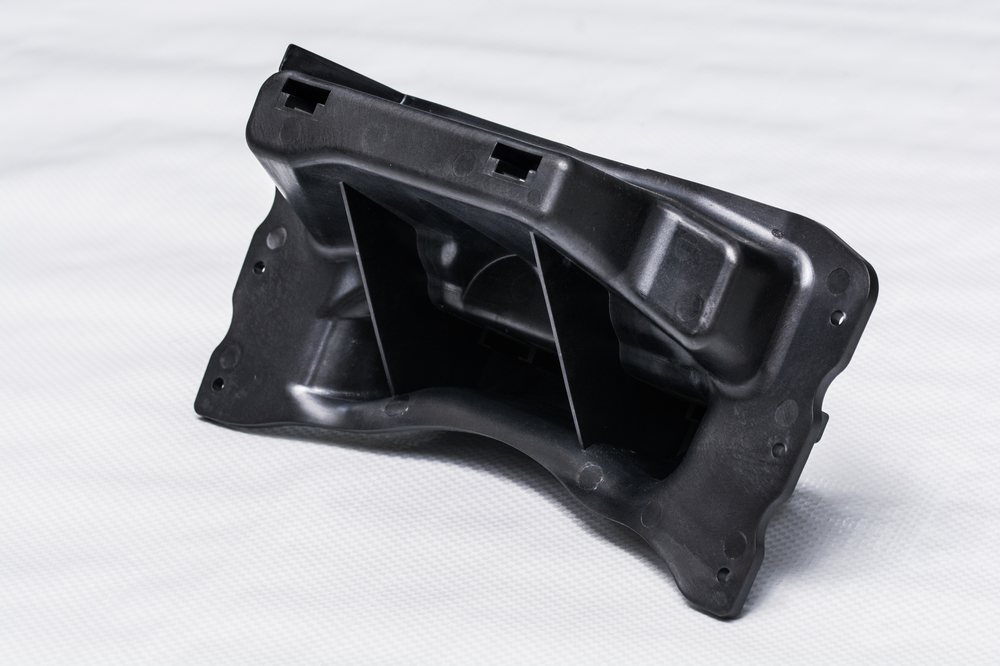
How each PEEK behaviour translates into a tool requirement.
Read more
Cost, lead time, steel grades, drying, minimum order quantity and grade selection.
Read moreSend STEP / UG / STP files by email or WeChat — you get material analysis, gating proposal, cycle estimate and mold price in one reply.
Request a Quote