When a PEEK part comes out wrong, the conversation usually starts at the press. It should start at the dryer and the mold temperature controller, because that is where most of these defects are actually created.
PEEK is hygroscopic. Under-dried material produces bubbles, silver streaks and a measurable loss of mechanical properties — defects that no amount of parameter tuning on the press will remove. Drying is specified per grade, verified, and not shortened because a deadline moved.
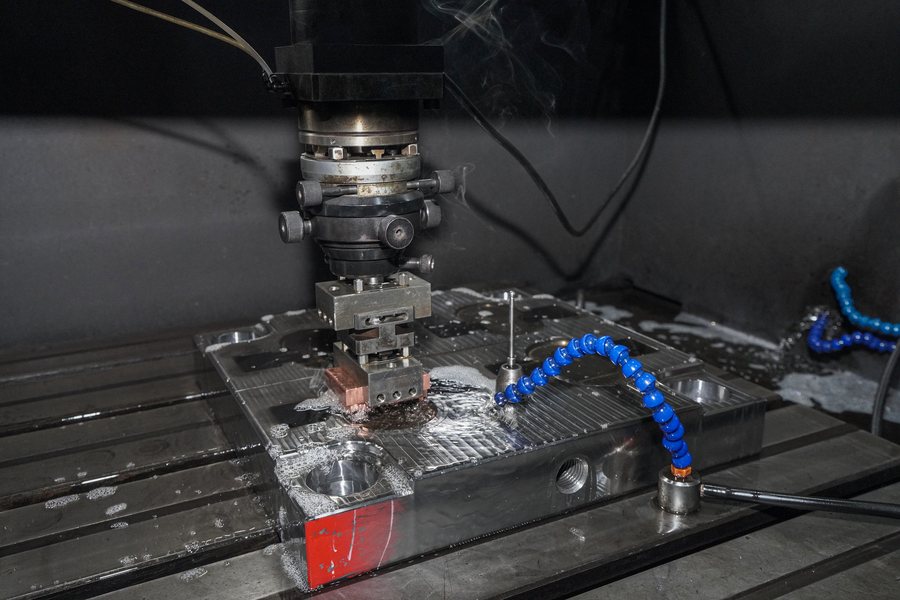
Crystallinity is decided by cooling. An uneven mold face means uneven crystallinity, which means the part warps and its properties vary from one side to the other. We run 160–220 °C oil temperature control with independent circuits for core and cavity, and hold mold-face uniformity within ±2 °C.
Precision parts are annealed at 200 °C for 2–4 hours and cooled slowly in the furnace. This releases internal stress and stabilizes dimensions and crystallinity. It is also the answer to the complaint that a precision PEEK part "moved after two days" — and it is the step most often omitted when delivery pressure builds.
Get drying, mold temperature and annealing right, and the press parameters become a fine-tuning exercise rather than a rescue operation.
Send STEP / UG / STP files by email or WeChat — you get material analysis, gating proposal, cycle estimate and mold price in one reply.
Request a Quote